
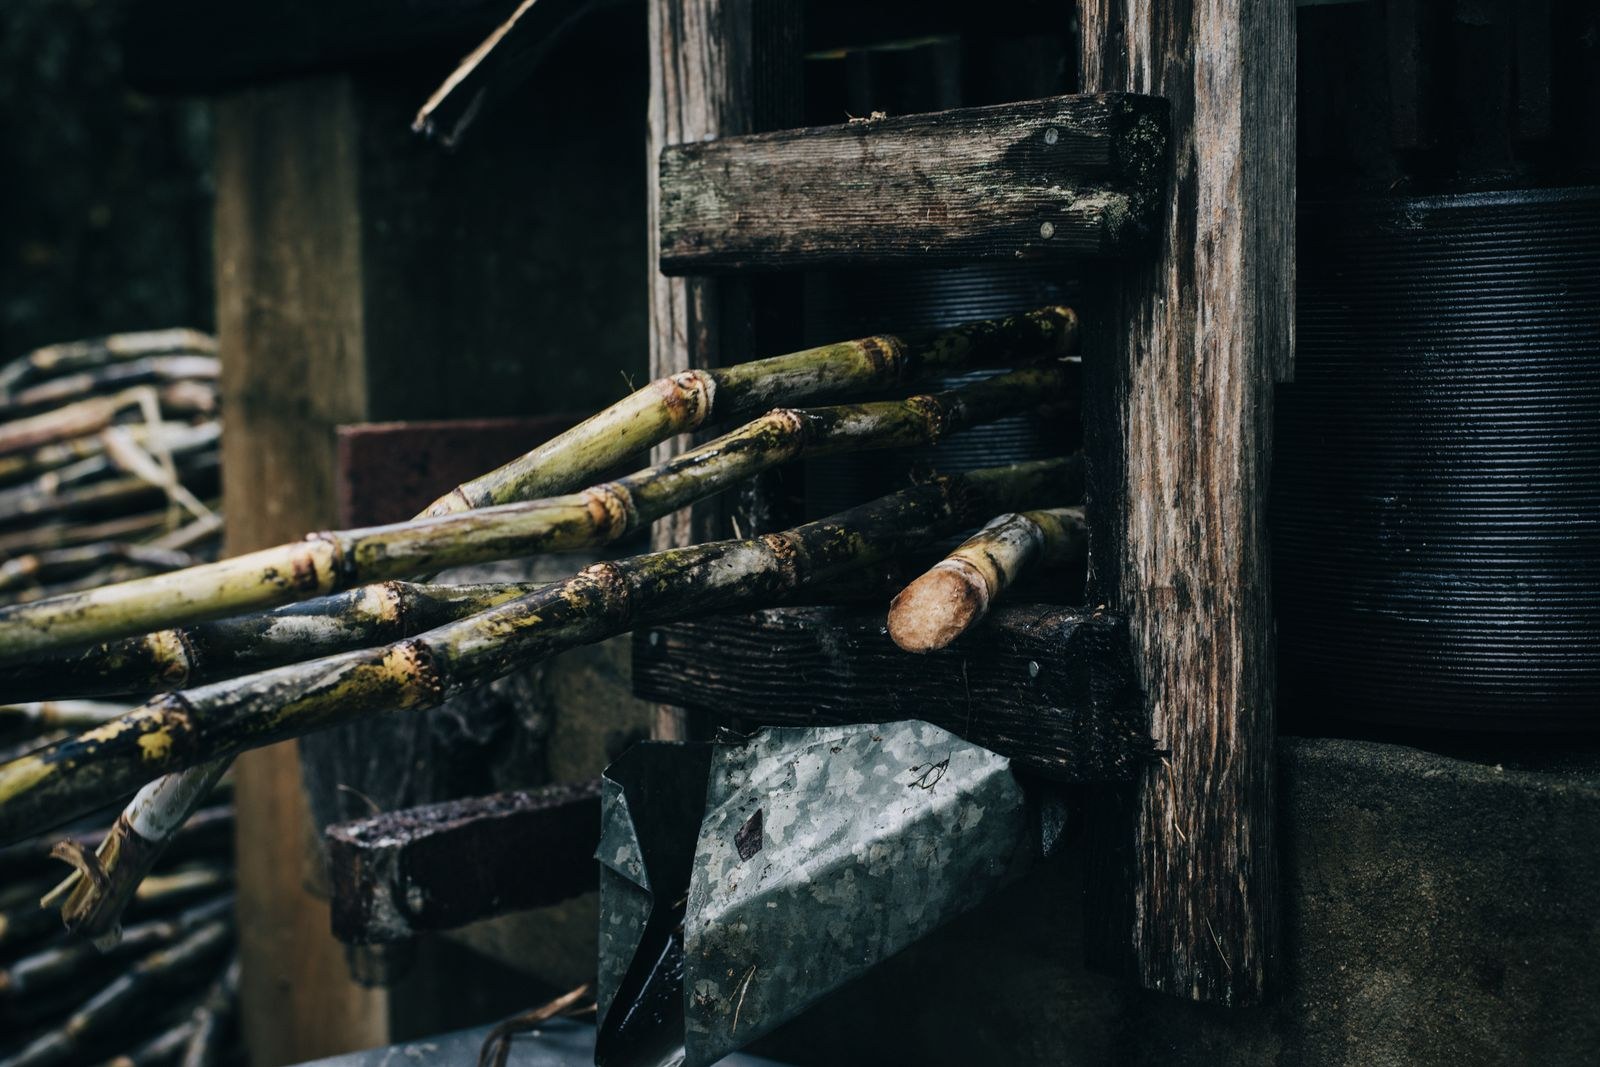
Sugarcane being fed into a press, photographed on site
Once a sugar mill raises the evaporation intensity at the concentration stage, foam surges on the syrup surface, the secondary vapour path is blocked by foam, vacuum falls away, and both the concentration rhythm and the syrup density come under pressure.
Chemi Tech has introduced the KM-750 series defoamer for sugar clarification and syrup concentration systems, with the dosage adjusted flexibly according to syrup brix and evaporation intensity. This grade resists high temperature, acid and alkali; it floats on the surface of the juice, breaking foam without affecting clarification and without interfering with syrup colour or purity. Customers can define the precise KM-750 dosage on the basis of measured data for evaporator level and the secondary vapour path.
Advantages of Chemi Tech Defoamers
Chemi Tech KM-750 series defoamer is configured for sugar and syrup concentration systems. High-temperature stability is strong, so defoaming capacity is retained even under the high temperatures of the evaporation stage; it resists acid and alkali, with no demulsification or separation in the acid-alkali environment of juice clarification; defoaming is fast, with the foam surging on the syrup surface removed quickly; compatibility with the juice is outstanding, with no precipitation and no floating oil, so syrup colour and purity stay stable; and the dosage is economical, adjusted flexibly to syrup brix and evaporation intensity so that the concentration rhythm stays stable and controllable.
Industry Pain Points and Solutions
Foam problems in syrup concentration stem mostly from the combined effect of surging during evaporation and incompatibility of the defoaming component, and the consequences are concentrated in two places: sliding vacuum and a blocked secondary vapour path.
Once vacuum slides, the heat transfer efficiency of the evaporator falls with it and the concentration cycle is repeatedly stretched. The KM-750 dosage is fixed by syrup brix, which holds the evaporator level steady and brings vacuum back into its normal band.
When the secondary vapour path is blocked by foam, liquid carry-over rises and the separation quality between condensate and syrup falls away. KM-750 resists high temperature, acid and alkali, breaking foam as it floats on the juice surface without carrying syrup away.
The steam loss brought by a stretched concentration cycle is ultimately converted into cost per ton of sugar. By narrowing the dosage range against changes in syrup brix and evaporation intensity, steam consumption per unit is reduced directly.
Typical Operating Conditions and Verification
Customer case: a sugar producer in Guangxi, for the syrup evaporation and concentration stage.
Evaporation intensity was not especially high, yet foam surged again and again through the crush-season peak. The background was rising liquid carry-over in the secondary vapour, with vacuum fluctuating around the critical line. KM-750 was set as the replacement scheme for the mill's concentration stage, with the dosage fixed by syrup brix. After the switch: the evaporator level fell back to normal; liquid carry-over in the secondary vapour dropped markedly; vacuum levelled out and the concentration cycle returned to its usual length.
Frequently Asked Questions
Does adding a defoamer at the sugar evaporation stage affect the colour and purity of the syrup?
What directly determines syrup colour and purity is the compatibility between the defoaming component and the juice. KM-750 has completed colour and purity comparison tests under syrup concentration conditions, and within the recommended range it neither precipitates nor floats oil, so syrup indices stay stable. The actual dosage takes syrup brix as its baseline, with evaporation intensity and concentration temperature set as corrections; Chemi Tech defines the adapted dosage through a parallel comparison of evaporator level and the secondary vapour path.