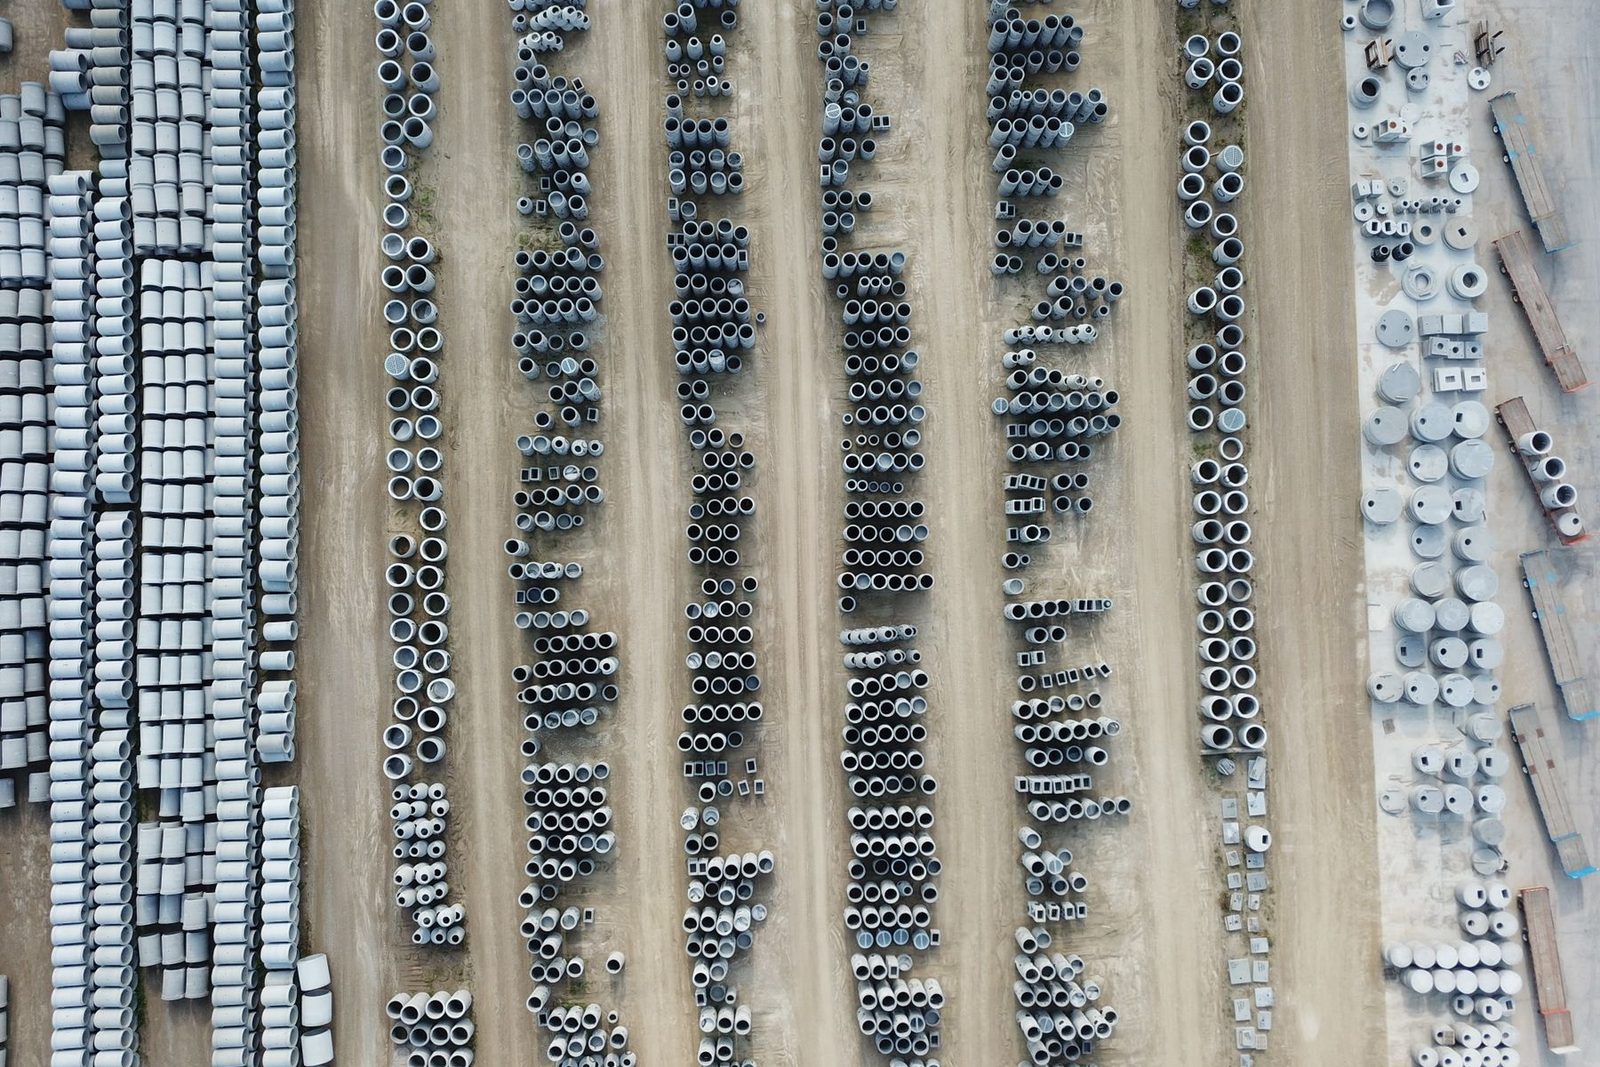
Concrete components and pipe stacks seen from above, bundles laid out in rows across the yard
At a precast plant, mineral-oil release agent foams in the mixing tank after dilution; the liquid film sprayed onto the steel mould carries fine bubbles, and after demoulding the component surface is left with a dense field of pinholes, while the hours of patching mortar and manual grinding stack into the month's overhead.
Chemi Tech supplies the KM-702 series of defoamers for mineral-oil release-agent systems in precast concrete; the dosage is adjusted by the agent's dilution ratio and spray pressure. KM-702 is a mineral-oil defoamer; it is excellently compatible in mineral-oil systems, and fine bubbles coalesce and rise as well. Set the measured foam-layer height in the mixing tank against the pinhole count on the component surface, and the fitted dosage for the KM-702 series settles naturally.
Advantages of Chemi Tech Defoamers
The Chemi Tech KM-702 series defoamer is configured for the release-agent preparation and spray stages of precast concrete. It is excellently compatible in mineral-oil systems, with no emulsion splitting or oil floating; foam breaking is fast, so floating froth in the tank clears before spraying; it handles fine bubbles well, coalescing and floating even sub-100-micron foam; it does not affect release-agent film formation, so after demoulding the mould face is clean and the component edges stay intact; alkali resistance is good, so it is not saponified and consumed in the alkaline cement environment; and the dosage is economical, graded by the release-agent dilution ratio, so the number of components sent for re-spray and rework narrows.
Industry Pain Points and Solutions
The foaming problem of mineral-oil release agent has its root mostly in the combined action of air entrained by high-speed stirring and the low surface tension of the emulsion itself, while spray atomisation breaks the fine bubbles up again, finally concentrating in two places: floating froth on the tank and pinholes on the component surface.
When the stirrer speed goes up, air is entrained into the emulsion and a layer of fine froth still floats on the tank after half an hour of standing. KM-702 handles these fine bubbles well, and the floating froth is held down before spraying.
The nozzle breaks the bubble-laden emulsion into droplets; the fine bubbles land on the mould, neither breaking nor coalescing, and after vibration they leave pinholes on the component surface. Spray atomisation pressure is another variable; by grading the KM-702 dosage against it, the liquid film on the mould tends toward flatness.
Pinholes must be patched one by one and then ground, adding labour per batch. With the dosage graded by the release-agent dilution ratio, the number of components sent for re-spray and rework falls, saving the patching and grinding labour.
Typical Operating Conditions and Verification
Customer case: a precast-component enterprise in Hebei, applied to the release-agent preparation and spray stages of composite floor slabs and stair flights.
After batching in the mixing tank, the floating froth on the tank still would not subside after half an hour of standing; fine bubbles were dense on the sprayed mould, and after demoulding pinholes concentrated on the same side of the component; the labour for patching mortar and grinding was counted separately by the day. Comparing the release-agent dilution ratio and atomisation pressure, the plant switched to KM-702 as the release-agent defoamer, the dose taken by component type and mould material. After it went in, the floating froth on the tank subsided before spraying; the liquid film on the mould tended toward flatness; the pinhole count on the component surface dropped markedly, and the rework-and-grinding hours came down.
Frequently Asked Questions
With defoamer added to the release agent, will it affect the component edges after demoulding and the mould cleanliness?
What decides this directly is whether the emulsion stays uniform at the spray terminal. KM-702 has completed comparative measured tests of foam-layer height in the mixing tank and pinhole count on the component surface in precast-concrete release-agent systems; within the recommended range the emulsion does not split or float oil, and after demoulding the edges stay intact with no sticky residue on the mould face. With the release-agent dilution ratio as the baseline and atomisation pressure and component surface area as further trade-offs, the fitted dosage is settled by the comparative verification of pinhole count and mould residue.